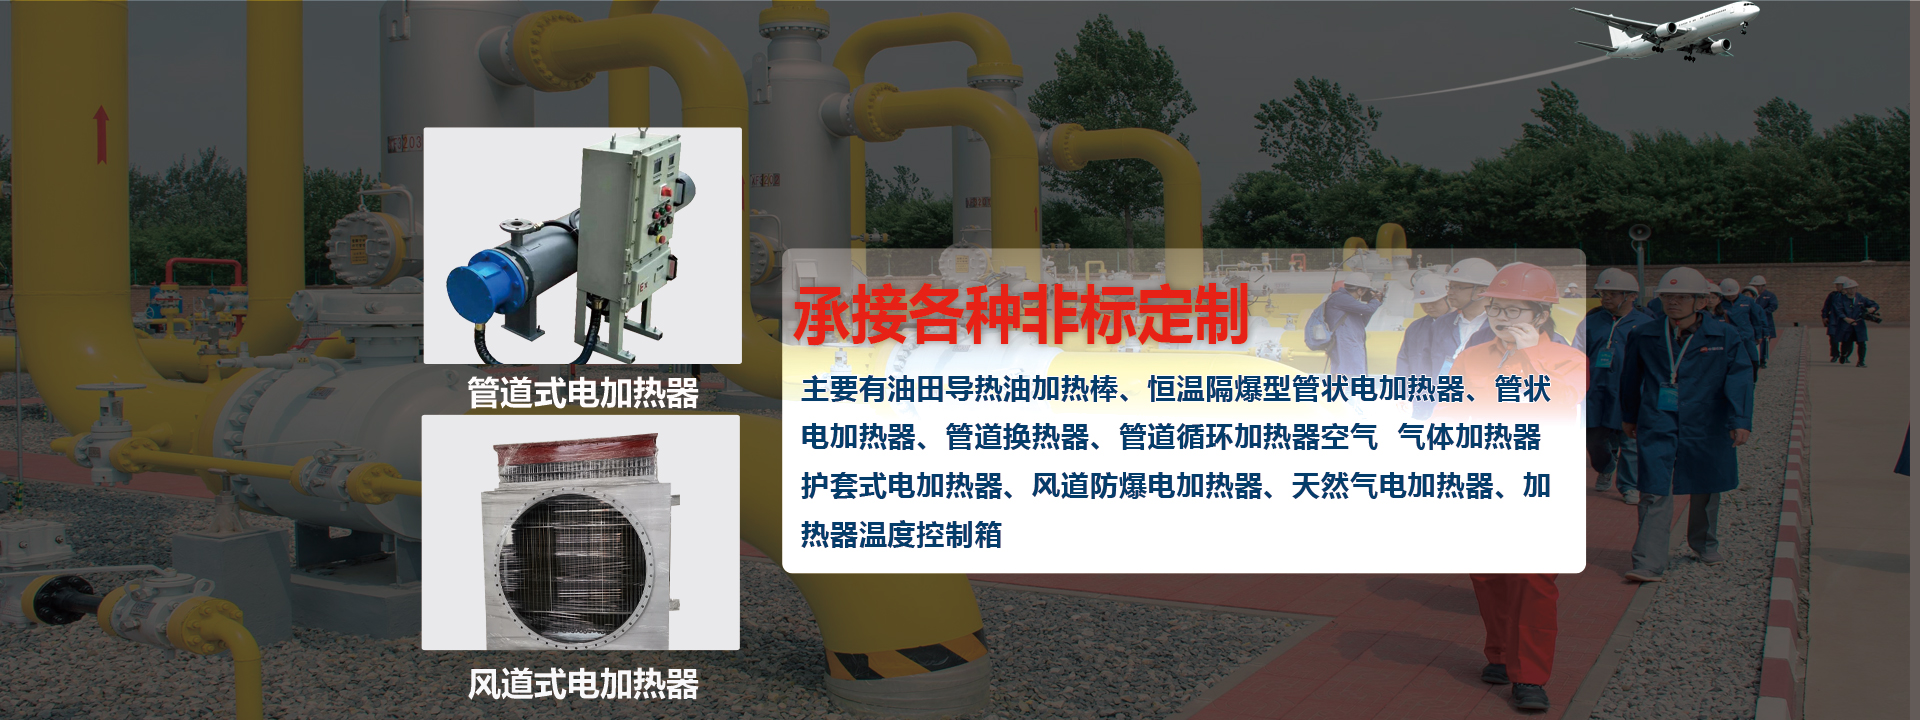
It achieves effective heating of fluid media while ensuring electrical safety by enclosing the resistance wire inside a metal tube (usually stainless steel) and filling it with thermally conductive insulating material (such as magnesium oxide). This design not only improves heating efficiency but also extends the service life of the equipment.
Main Features
High Efficiency: Due to its compact design and the use of high-quality materials, the sheathed electric heater can quickly transfer heat to the heated medium, providing a high energy efficiency ratio.
High Safety: The electric heating element is completely isolated from the outside, effectively preventing electric leakage accidents and ensuring safety during use.
Strong Corrosion Resistance: The sheath made of stainless steel or other corrosion-resistant materials makes this heater particularly suitable for corrosive environments or heating corrosive liquids.
Sturdy and Durable Structure: Reasonable design and careful material selection give the sheathed electric heater a long service life.
Easy Maintenance: Due to its simple structure and easy disassembly, daily maintenance and care are very convenient.
Application Fields
Chemical Industry: Used for heating materials in chemical reaction kettles or as temperature control components in process flows.
Oil and Natural Gas: Suitable for heating treatment processes of crude oil and its products to improve fluidity and processing efficiency.
Food and Beverage: Involved in disinfection, sterilization, evaporation, and concentration processes during production.
Power Engineering: Provides necessary preheating services for various systems in power stations.
Other Fields: Including but not limited to pharmaceuticals, textiles, papermaking, etc., where precise temperature control and efficient heating are required.
Development Trends
With technological advancement, sheathed electric heaters are also evolving. The development of intelligent control systems makes the heating process more precise and controllable; energy-saving and environmental protection requirements drive manufacturers to develop more efficient heating technologies and materials; while the growth of customized demand promotes product diversification to meet the special needs of different users.
In summary, with its unique advantages, the sheathed electric heater plays an important role in many fields and continues to innovate and improve with technological development, contributing to the progress of various industries.